The Slide That Set Everything Up
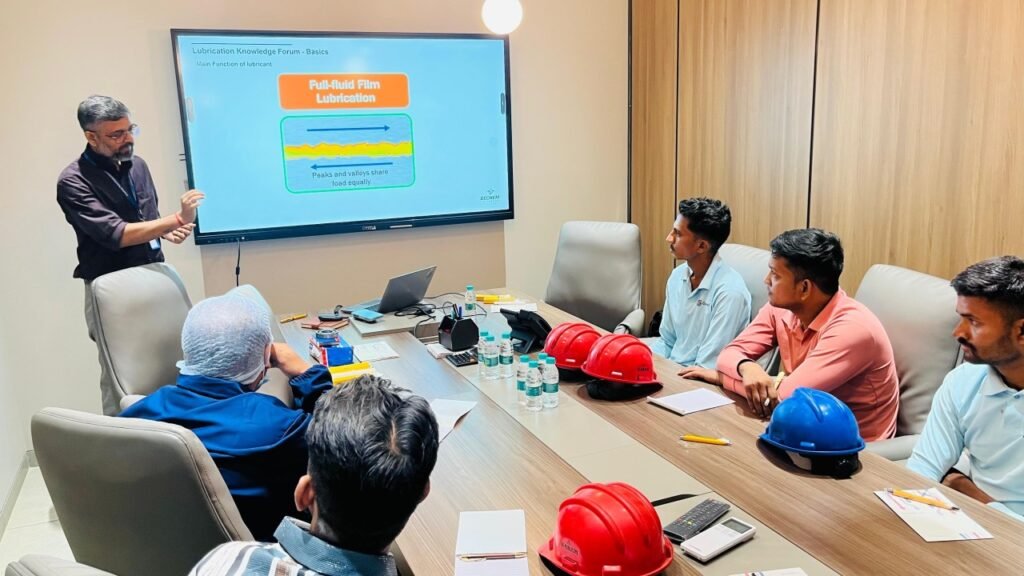
I had opened the session with a slide on Full-fluid Film Lubrication — one of my favourite to start with, because it cuts straight to the why of lubrication.
The slide showed something deceptively simple: two surfaces in relative motion, separated by a fluid film. Beneath the film, the microscopic peaks and valleys of each surface — and the caption read: “Peaks and valleys share load equally.”
I let that sit for a moment.
Then I asked the room — “What happens if this film breaks down? If the oil between these surfaces is too thin, or too thick for the speed of motion?”
A few uncertain looks. One engineer ventured — “The surfaces touch?”
“Exactly. Metal meets metal. And that’s where wear begins.”
That single question pivoted our entire session. Because the answer to it lies not in which grease brand you pick, or which thickener you prefer — it lies in something far more fundamental:
The base oil viscosity.
“Sir, Isn’t Grease Just… Thick Oil?”
One of the youngest engineers in the room asked this, almost hesitantly. And I told him — that’s actually a brilliant starting point.
A grease is essentially a base oil held in place by a thickener, with additives doing the performance heavy lifting. The thickener gives grease its structure — it’s what keeps it from flowing away like oil. But here’s what most people miss:
The thickener holds the oil. The oil does the lubricating.
So when we talk about viscosity in a grease, we’re really talking about the base oil viscosity — the viscosity of the oil that will be released at the contact zone, between the rolling or sliding surfaces, when the grease is worked under load and heat.
Get that wrong, and no amount of premium thickener or fancy additive will save your bearing.
So What Exactly Is Base Oil Viscosity?
Viscosity is simply a fluid’s resistance to flow — its “thickness,” if you will. In grease, the base oil viscosity is typically expressed as kinematic viscosity in cSt (centistokes) at 40°C and 100°C.
A grease can have a low base oil viscosity (say, 22–46 cSt at 40°C) or a high base oil viscosity (460–1500 cSt at 40°C) — and each serves a fundamentally different purpose.
I drew a simple table on the whiteboard:
| Base Oil Viscosity | Typical Application |
| Very Low (15–46 cSt) | High-speed spindle bearings, precision instruments |
| Low to Medium (68–150 cSt) | General purpose bearings, electric motors |
| Medium to High (220–460 cSt) | Gearboxes, heavily loaded slow-speed bearings |
| Very High (>460 cSt) | Open gears, wire ropes, sliding surfaces I
The room went quiet for a moment. Then one engineer looked up and asked — “So if we use a high viscosity grease on a high-speed bearing, what happens?”
Exactly the right question. And I pointed back to the slide still on the screen behind me — that full-fluid film diagram.
“Think about it this way. That film we saw? At high speed, the surfaces are moving fast. If your base oil is too viscous, it generates too much internal friction just trying to shear through itself. The film doesn’t protect — it overheats. You’re fighting the lubricant, not working with it.”
The Speed–Viscosity Relationship: The Core of the Conversation
This is where things got really interesting.
I explained the concept of the DN value — Bearing Bore Diameter (mm) × Speed (RPM). This is a quick, practical indicator of how fast a bearing is running.
High DN value → High speed → You need lower base oil viscosity
Low DN value → Low speed / high load → You need higher base oil viscosity
Here’s the logic behind it:
At high speeds, the bearing surfaces are moving fast and generate significant churning heat. A high-viscosity base oil at these speeds creates excessive fluid friction, heat buildup, and energy loss — the grease literally works against the bearing. You end up with a hot bearing, premature grease oxidation, and eventual failure.
At low speeds, the surfaces move slowly and there’s very little hydrodynamic lift — the oil film that separates the surfaces is hard to maintain. Here, a thin, low-viscosity oil simply cannot build an adequate film. Metal meets metal. Wear accelerates.
I looked at the team and said: “The job of the base oil is to form a film between surfaces. Too thin for the load and speed, it breaks down. Too thick for the speed, it creates heat. Your job is to find the sweet spot.”
Temperature: The Variable That Changes Everything
One of the senior engineers in the room — quiet until now — raised his hand.
“Sir, we also work in environments where temperature swings are significant. Outdoor equipment in winter, furnace-side equipment in summer. Does that change things?”
Absolutely it does. And this is where the concept of Viscosity Index (VI) becomes important.
Viscosity changes with temperature — all oils thin out as they heat up and thicken as they cool down. An oil with a high Viscosity Index resists this change better — it stays relatively stable across a wide temperature range.
For equipment operating across wide temperature extremes:
Synthetic base oils (PAO, Esters) offer much higher VI than mineral oils
They also perform better at very low temperatures (low pour points) and very high temperatures (better oxidation resistance)
So when your application sits near a furnace or runs outdoors through a cold winter, the base oil type — not just its viscosity grade — becomes equally critical.
The Mistake We See Too Often on the Shop Floor
By this point, the room was buzzing. And I decided to share the most common mistake I’ve seen in plants over the years.
Using the same multi-purpose grease for every application in the plant.
I understand why it happens — simplicity, procurement convenience, fewer SKUs. But here’s the cost of that decision:
A multi-purpose grease with 100–150 cSt base oil applied to a slow-moving, heavily loaded pin joint at 50 RPM is setting you up for adhesive wear.
The same grease applied to a high-speed electric motor bearing running at 3000 RPM is causing energy loss, heat, and oxidation failure.
Two completely different failure modes. One common culprit — wrong base oil viscosity for the application.
A Simple Framework I Left Them With
Before wrapping up, I put a simple decision framework on the board:
Step 1 — Know your speed: Calculate DN value or refer to the OEM recommendation.
Step 2 — Know your load: Is it light, moderate, or heavy? Shock loads? Oscillating motion?
Step 3 — Know your temperature: Operating range? Ambient extremes?
Step 4 — Match the base oil viscosity: Use the speed-viscosity relationship as your anchor.
Step 5 — Then choose your thickener and additives based on compatibility, water resistance, and application requirements.
Most people start at Step 5. Start at Step 4 — and everything else becomes more logical.
Closing Thought
As the session wound down, the young engineer who had asked “isn’t grease just thick oil?” walked up to me and said — “Sir, I never realized there was so much inside a grease can.”
That moment, right there, is why I love these shop floor conversations.
And it all started with one slide. A simple diagram of two surfaces, a fluid film between them, and a line that said — peaks and valleys share load equally. When that film is right, everything is right. When it isn’t, everything downstream fails.
Grease is often treated as a commodity — something you buy by the kilogram and apply by habit. But lubrication is engineering. Every bearing is asking you a question about its speed, load, temperature, and environment. The grease you select is your answer.
And base oil viscosity — that’s the grammar of that answer. Get it wrong, and even the most expensive grease in your store will let you down.